Computer Vision in Manufacturing: The 4th Industrial Revolution
Computer Vision is revolutionizing Manufacturing. Learn how it is powering the next generation of manufacturers and establishing the 4IR.
Carolina, Catalina
In our post on computer vision in retail, we went over seven of the most exciting uses of Computer Vision in that industry. Now let's take a step back and look at what Computer Vision has to offer in Manufacturing.
We can't do that without looking at the Fourth Industrial Revolution (4IR), also known as 'Industry 4.0'. It is reshaping the manufacturing industry by bringing AI into its processes to make them more efficient. McKinsey reports that by 2025, the technologies behind this revolution could add up to $3.7 trillion in value.
A 2020 McKinsey survey on the state of AI found revenue increases and lower costs at companies that used AI in at least one function. Its examples of AI use cases in manufacturing and logistics included yield, energy, and throughput optimization, predictive maintenance, logistics-network optimization, inventory, and parts optimization.
Who are the manufacturing leaders in the 4IR?
In 2018, the World Economic Forum launched the Global Lighthouse Network. This ongoing research project brings together the pioneers of manufacturing innovation. These companies lead the way in adopting 4IR technologies, and they keep raising industry benchmarks. They are moving away from old, manual manufacturing and toward a smart and advanced manufacturing model.
Why bring a wide range of technologies (like computer vision) into the manufacturing industry? The main goal is to boost productivity and other key performance metrics. In any industry, this can be achieved by transforming manufacturing processes through digitalization and automation.
Industry leaders report positive results from early adoption of 4IR technologies across many manufacturing metrics. These are the ones that stand out:
- Increment in overall equipment effectiveness
- Deviation drop
- Cost of scrap diminution
- Cut back in human resources for inspection and validation
- Less unexpected breakdowns
- Decrement in defects per million
- Workforce productivity raise
- Decrement in customer complaints
- Increment in units produced per hour
- Extension of lifespan of equipment
- Labor efficiency boost
- Production time gain
- Cost of goods sold reduction
- Improvement of asset utilization
- Logistics cost cutback
- Rework cost decrement
- Performance growth
The lighthouses of manufacturing: what powers them?
These ‘Lighthouses’ come from very different corners of manufacturing. Still, they all focus on the same thing. They make the most of the technology they have to raise quality without losing efficiency. In the end, that is what keeps driving revenue.
Their key innovations include computer vision-powered inspection and predictive maintenance. They also use AI-enabled automation of quality management, 3D printing, big data analytics and real-time quality control for machining, among many others.
Computer vision as a part of the revolution
Manufacturing Lighthouses use AI to keep thriving in an industry that still depends a lot on people. As in retail, the human factor involves a cost because of the nature of the work. It is hard to track many variables at once, people make mistakes, and in this industry there is the added cost of keeping workers safe on the job.
The pandemic also showed why the human factor in manufacturing matters. Years on the job bring know-how that is hard to replace. And a company is exposed when its workers can't be on site.
The solutions that AI and Computer Vision bring help overcome these limits. They also help a company make better use of the people it already has.
Computer Vision helps manufacturers do more and fix weak spots in any industry. That is why the industry leaders trust this technology to keep scaling up innovation.
Custom computer vision algorithms in manufacturing turn visual data from daily work into action. That is how a plant reaches its target KPIs.
Four areas where computer vision has the most significant impact
Computer Vision has limitless potential, but four parts of a manufacturer's operations gain the most from it.
Quality assurance
Quality is one of the industry's top performance metrics, so it is always the main thing to improve. It cuts across every process and line of business. When it is ignored, the costs far outweigh the price of a quality management system. For manufacturers, those costs come from rework time, repairs, recalls, scrap, inspections, warranty charges, and late delivery penalties.
To avoid the costs of poor quality, manufacturers must invest in good, reliable tools to ensure the quality of the whole pipeline, from raw materials to the final product. Computer Vision plays a vital role here. It checks each part and the finished product. Defect detection by automated inspection reaches two main goals:
- No subtle defect goes unnoticed
- Automation allows for consistency of criteria regardless of the workload
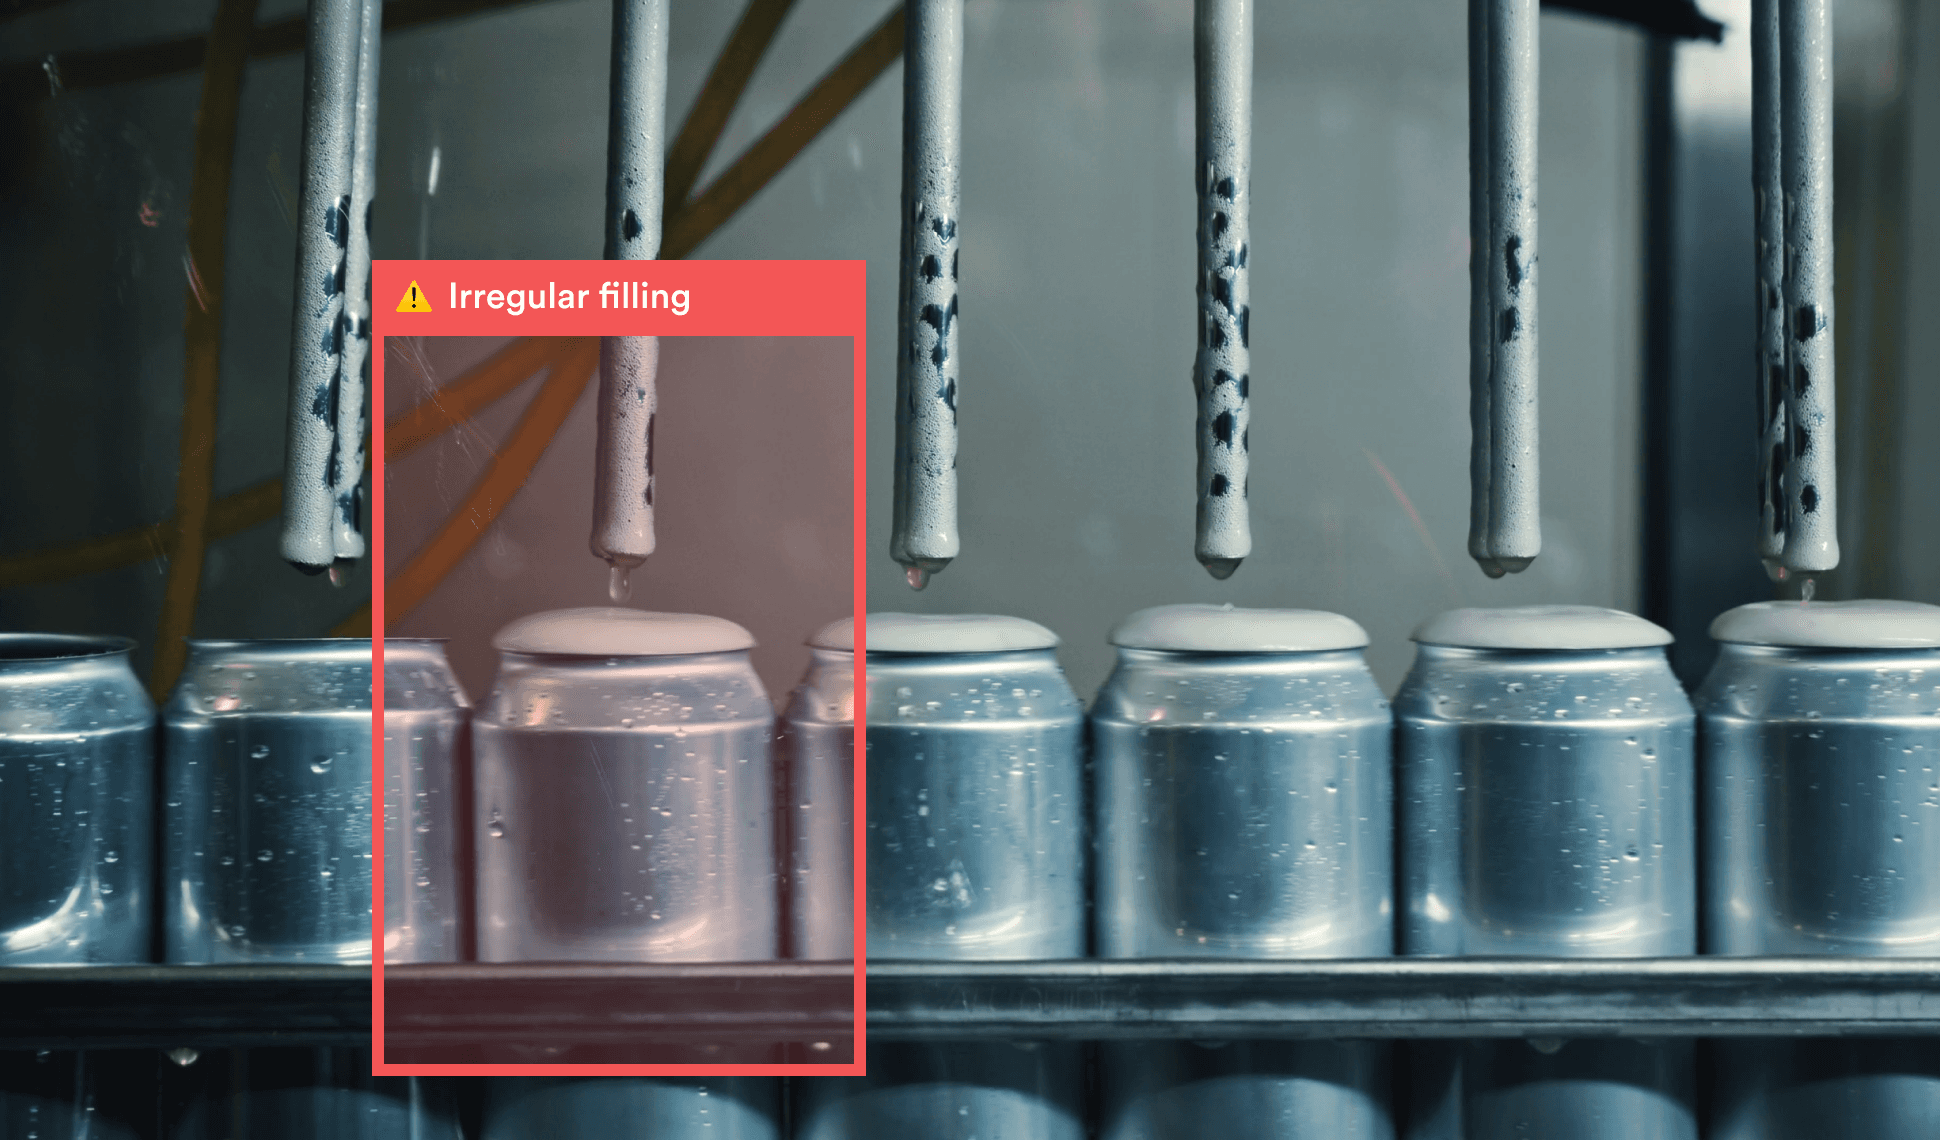
A quality control system built on Computer Vision-powered cameras can find errors and sort them by type. Based on the defect, a product can take a different route before it moves on to the next stage. This sorting also shows the weak points of the production process, so you know where to improve.
Catching faulty products and bad raw materials early in the line reduces the chances of recalls. That way, manufacturers avoid the additional costs of shipping faulty goods. They also avoid trouble in the sales pipeline and damage to customer loyalty.
Cameras pick up specific patterns when they inspect an item. From there, image processing algorithms can tell what counts as an error and send an alert. They can also catch trends. A reading may sit inside the allowed range but close to its upper or lower limit. That can point to a problem if no one acts on it.
Faulty products are not the only concern of automated quality control. Today, the look of the final product also matters for sales and for the manufacturer's reputation.
At this stage, manufacturers must ensure that packaging standards are met. That covers barcodes and text. It also means labels and compliance marks must be easy to see and in the right place. Here, the role of Computer Vision in Manufacturing is clear. It finds and pulls aside items that miss the standards before they leave the plant, saving the manufacturer considerable costs.
Last, steady and strict quality checks help manufacturers earn quality and good manufacturing certificates. These show that a plant meets a set of manufacturing standards. Some goods, such as drugs or medical devices, can't be sold in highly regulated markets without these certificates.
Production
Designing Computer Vision algorithms to improve a task that people would otherwise do by hand takes a team. Process and production engineers work with Computer Vision experts. They share clear goals they can measure, and they know how those goals affect the manufacturer's KPIs.
Computer vision algorithms can handle predictive maintenance of manufacturing equipment and fleet assets. The model watches visual signs such as rust, shape, or surface to spot errors or departures from the standard. You can train it to be as accurate as you need. It learns to detect known or unknown signs of wear that could lead to a breakdown of costly equipment.
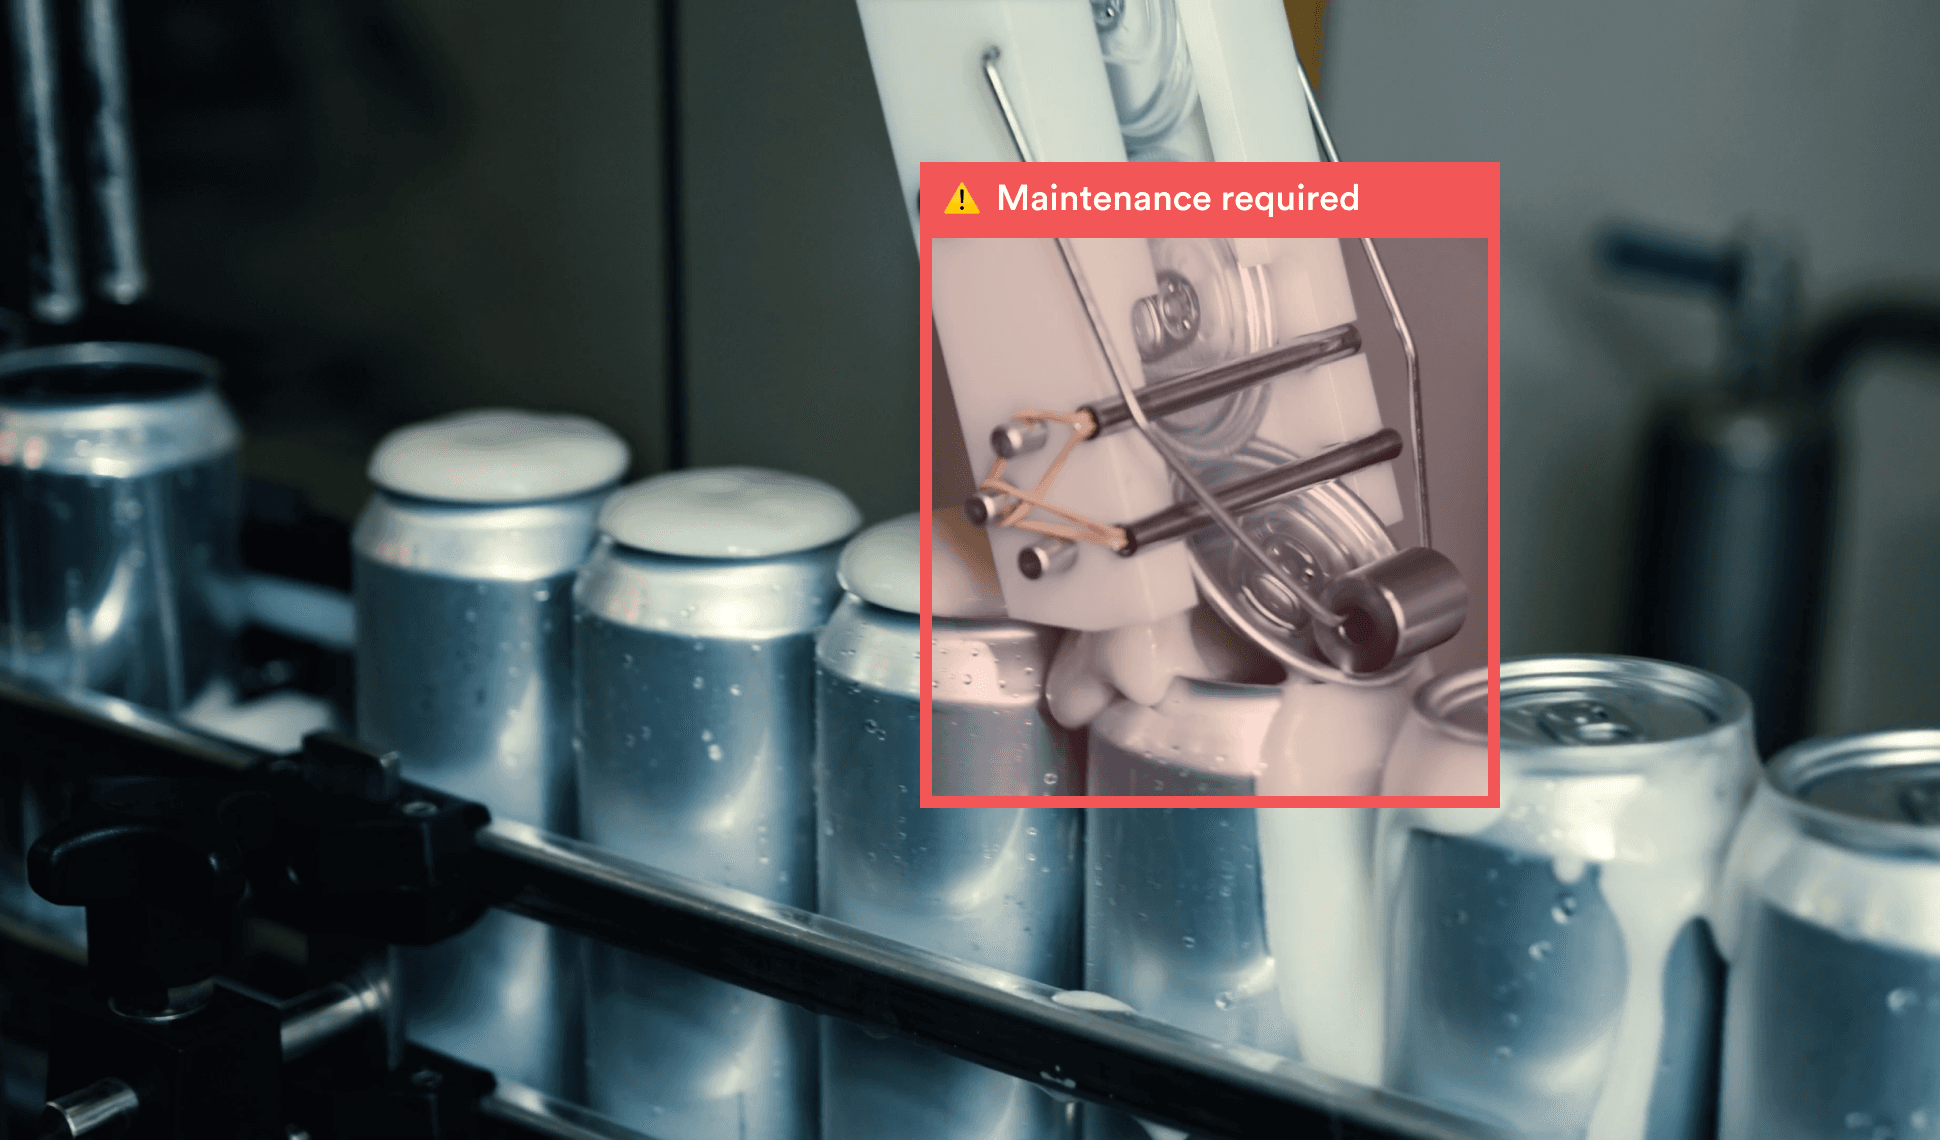
Predictive maintenance lets manufacturers analyze how their machines perform. With that input, workers stop replacing parts that don't need it. Manufacturers no longer pay to take a machine apart to swap a part that could have run six more months. As a result, predictive maintenance cuts the yearly maintenance bill and helps estimate how long each part will last.
Once the system finds an error, it sends a remote warning or shows an alert on the right andon board. Workers can then decide in time what to do, based on the type and severity of the error.
As a result, the manufacturer avoids losses in equipment and extends the life span of their assets. Most important, if production has to stop, they can plan for it. The next processes keep running and unplanned downtime goes down.
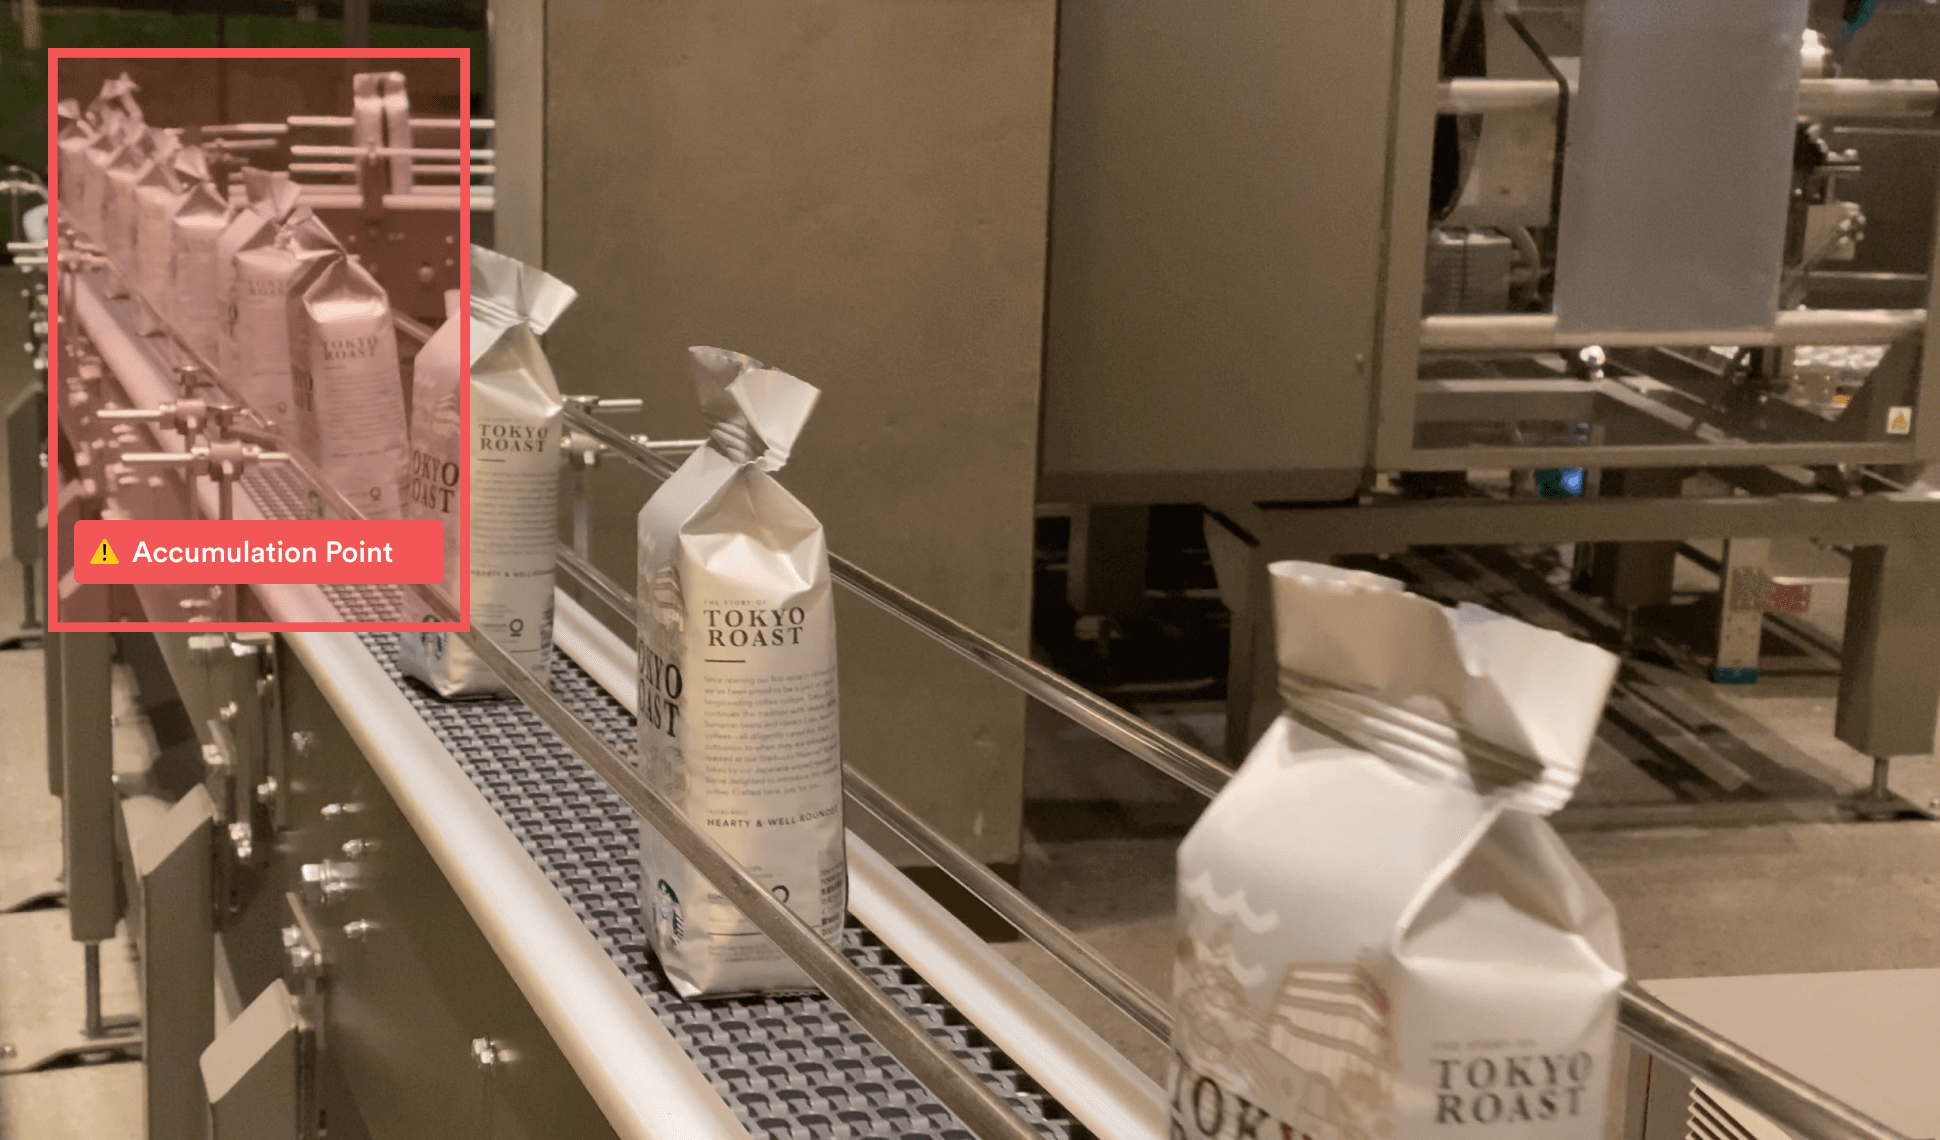
Object detection, one of the computer vision techniques, can also sort and count items. That is a big help for the visual inspection of manufacturing processes. It matters especially in the pharmaceutical industry. There, an incomplete blister pack or any change in the final product could have severe effects on clients. Manufacturers could also face additional legal costs if defective product liability lawsuits occur.
Manufacturers that do precise laser or rotary die-cutting can also use Computer Vision to cut the cost of scrap. The models learn from images or videos that set the gold standard. They then guide the machines the same way every time, reducing variability and the cost of scrap.
Safety & compliance
The physical integrity of workers should be a priority for every company, whatever the work. In the manufacturing industry, there is no margin for error when it comes to the safety of human capital.
So manufacturers must keep track of compliance with the protocols that keep workers safe. They also need to watch accident-prone areas, emergency exits that must stay clear, and zones that must stay empty for traffic.
Usually, one worker watches several cameras aimed at different work stations, with people and heavy machines moving around. No one can stay alert all the time and handle that many signals without making mistakes.
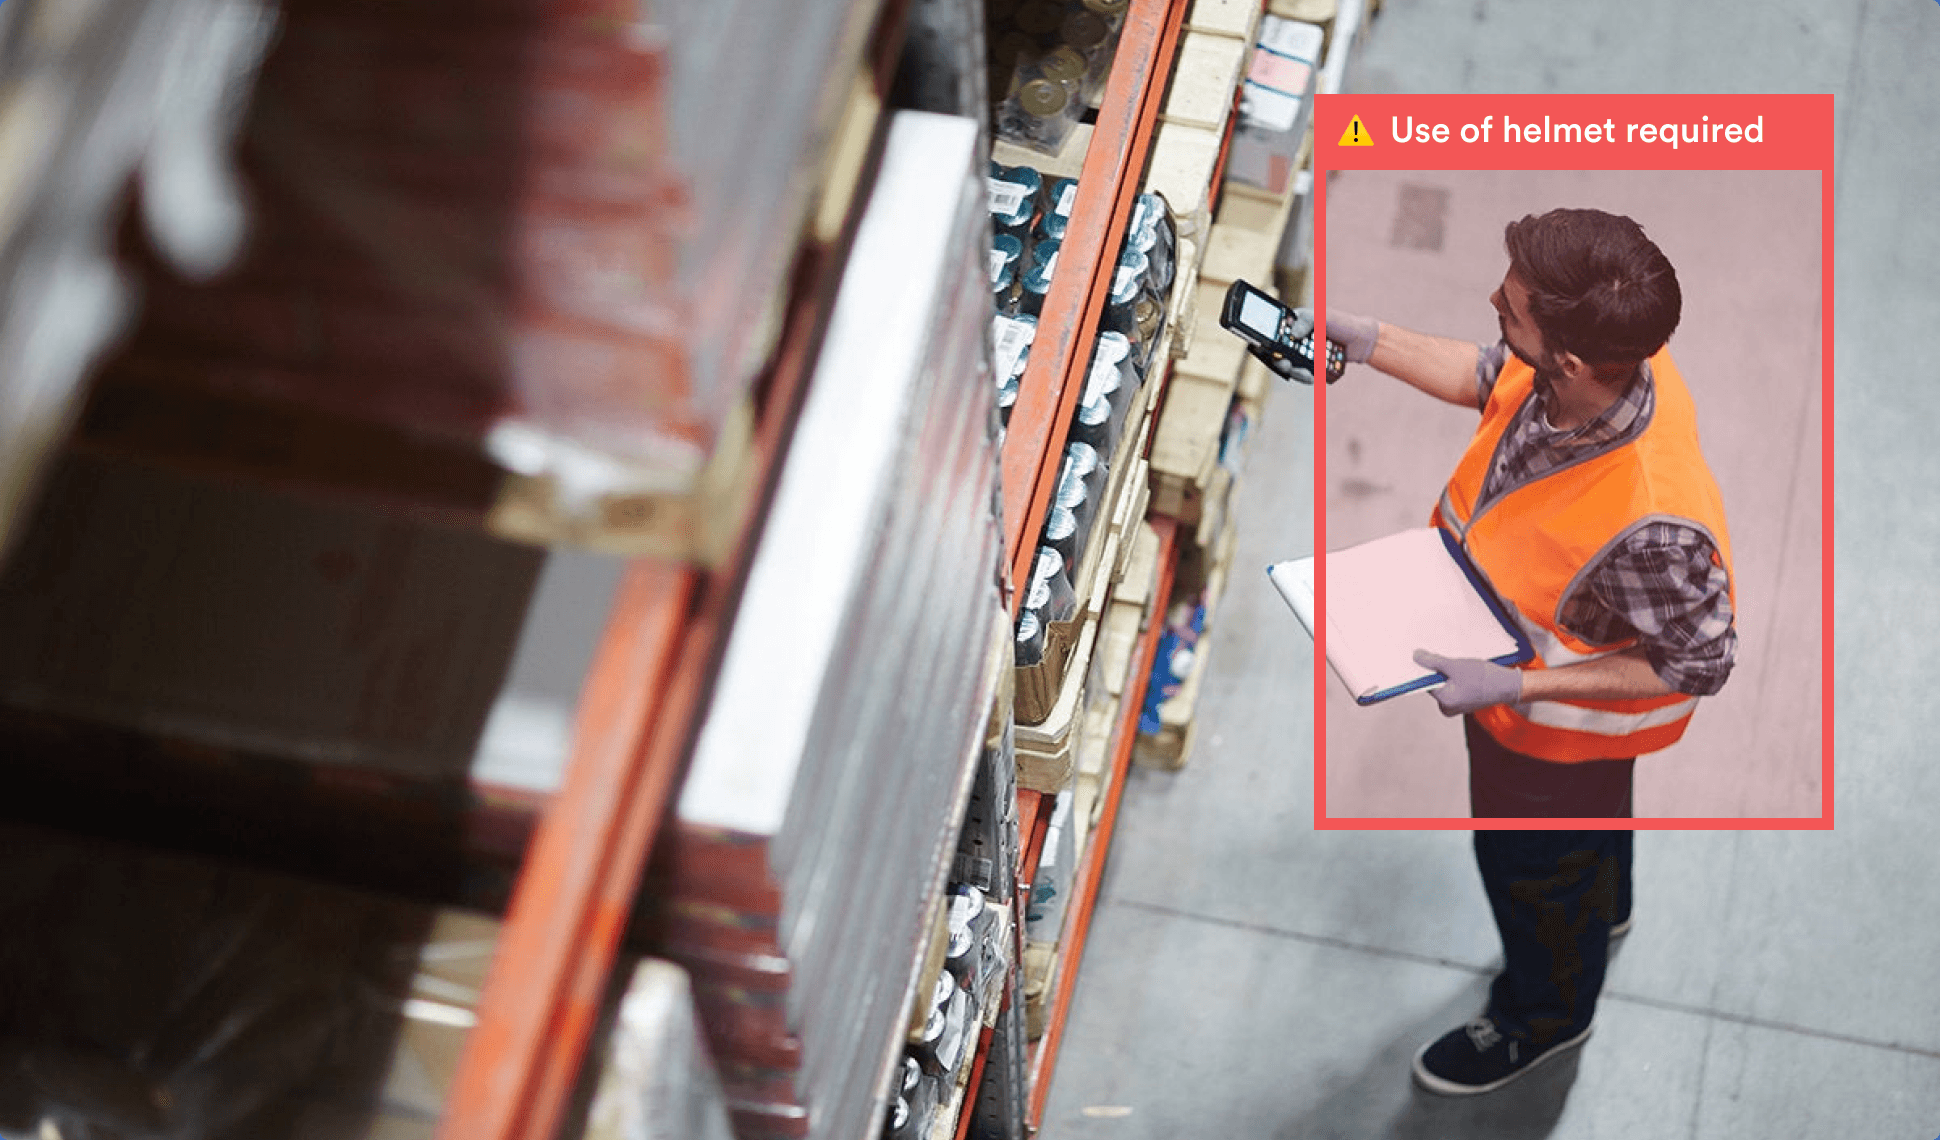
Workers in this industry can risk injury during manual checks or repairs, or while they walk through hazardous zones in plants and warehouses. Sometimes, on purpose or not, workers skip safety rules or the use of personal protective equipment (PPE) like helmets, masks, or safety glasses. That puts the worker at risk. In plants that make food or need a sterile space, it can also become a public health issue.
When human monitoring of compliance fails, worker well-being suffers. Companies can also face fines for breaking the rules. Here, computer-vision-powered monitoring of plant conditions is an excellent fit for manufacturers. It checks the use of PPE around the clock and runs remote checks in a manufacturing plant. No worker has to be there in person, and the checks have the accuracy only software can reach.
Logistics & Inventory
Everything from buying raw materials to shipping the final product is also in scope for Computer Vision in manufacturing. Logistics is key to short lead times and to meeting the needs of clients inside and outside the company. Many choices about storage space and transport routes also help avoid incurring additional costs and delays in the flow of products.
Manufacturers can set up procedures for organizing their inventory, then use them to feed and train computer vision models to achieve vision-based inventory control. Once in production, the models can take over these dull, repetitive and error-prone tasks and do them better than people.
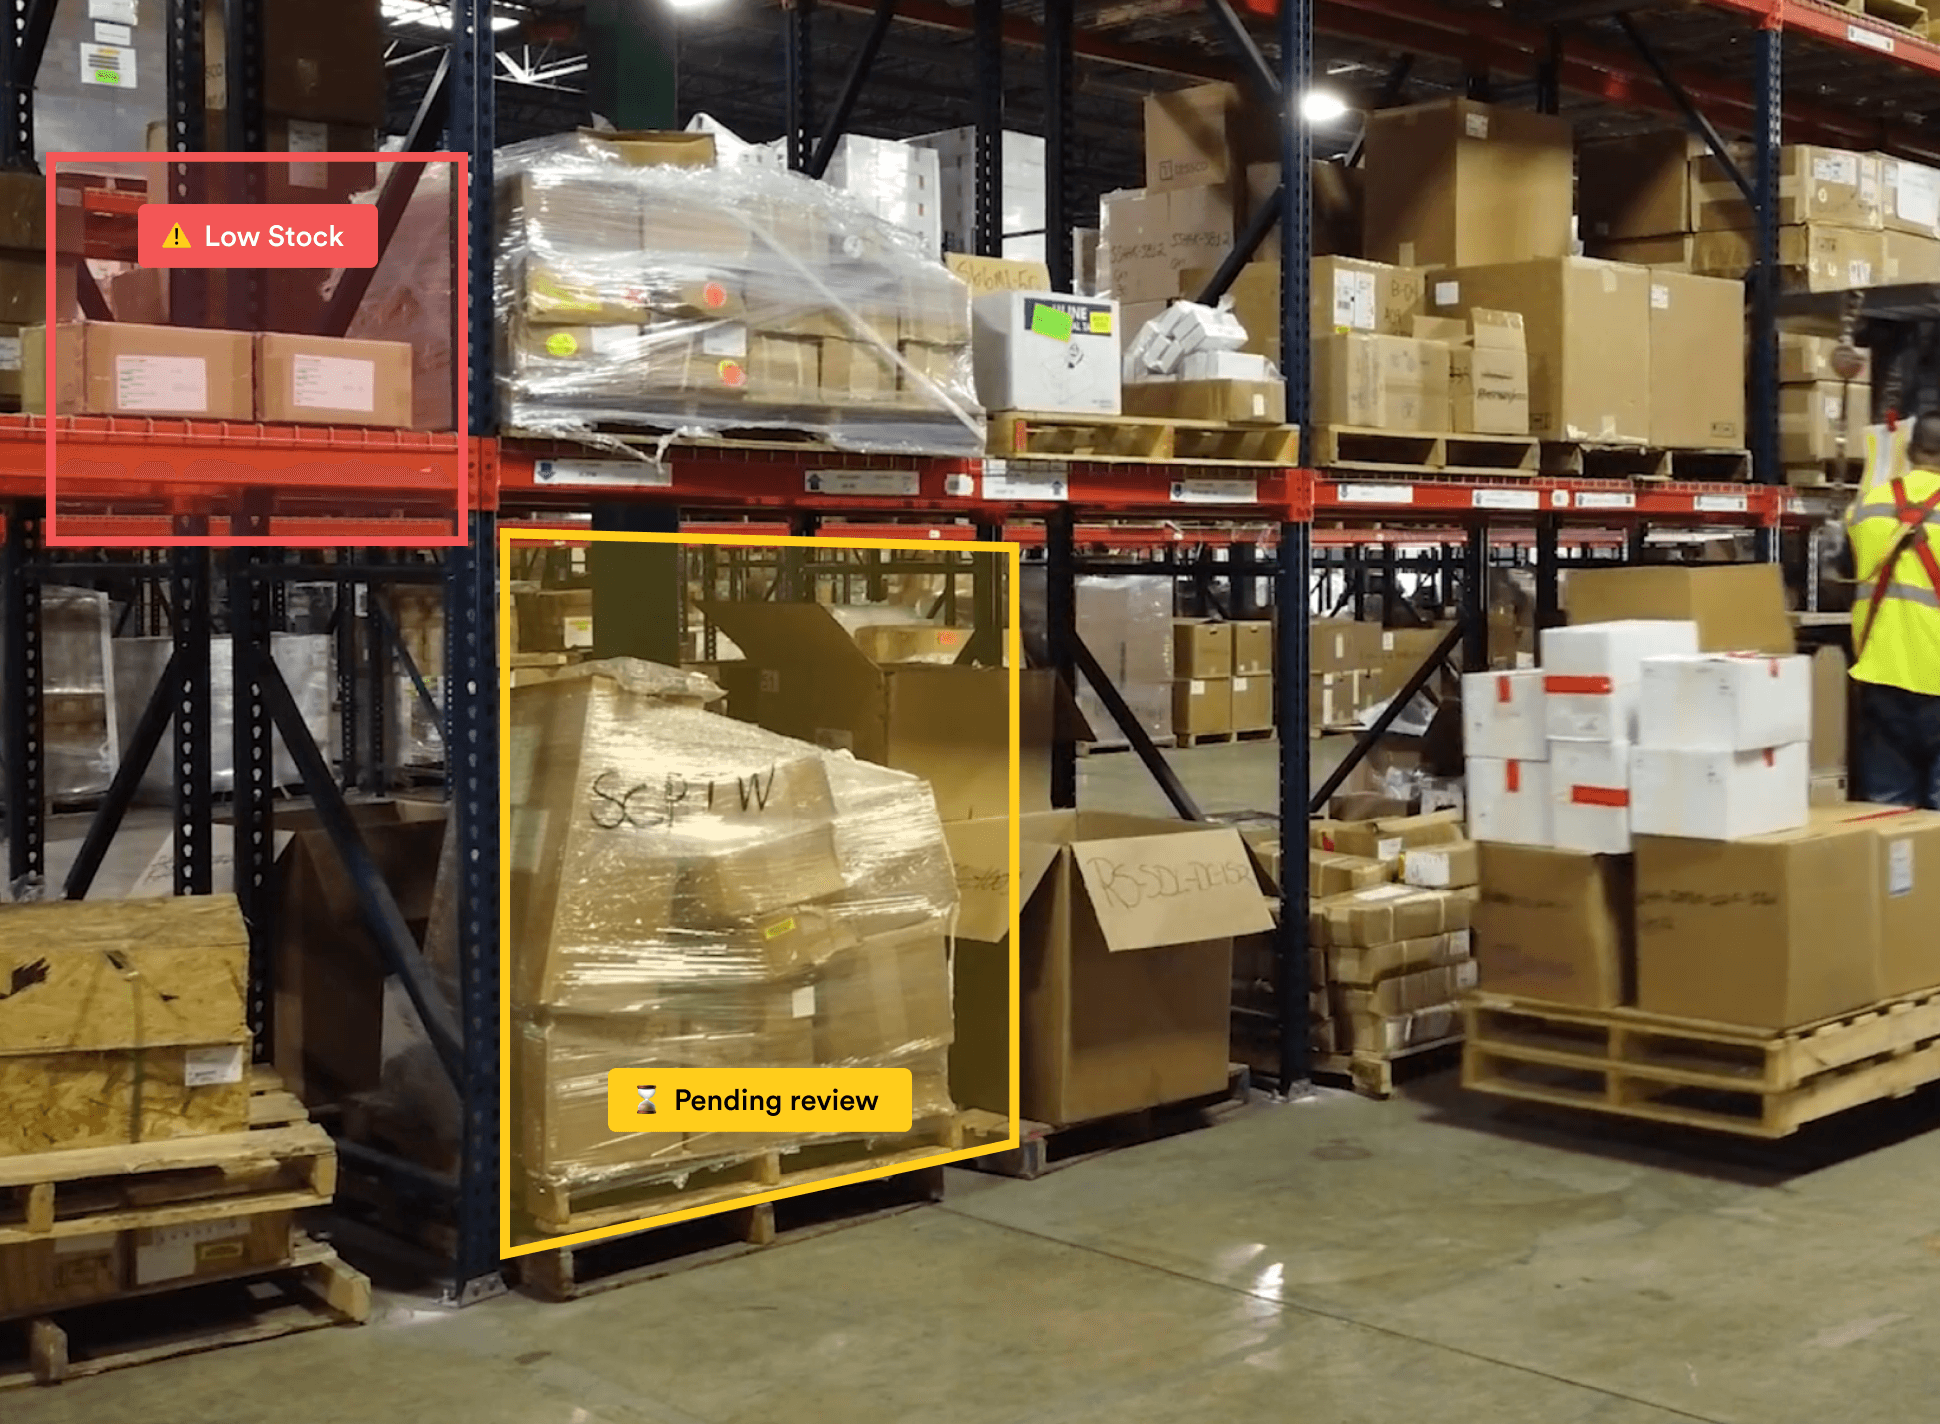
Custom computer vision algorithms built into the manufacturer's inventory management system help find the exact location of each item. When cameras read a label, QR code, or barcode, the system can identify, track and trace an object without fail. When packages are sorted and moved by size or weight, the system sends an alert if something goes wrong. Workers can then reroute the package.
To keep goods flowing, video analytics helps warehouse managers make good use of the space they have. It also keeps a record of warehouse work. The algorithms can watch how full traffic and storage areas are to detect and recognize bottlenecks.
Computer vision-powered cameras also monitor parking lots and loading docks. That helps avoid delays and extra operating costs when you plan loading and shipping.
Closing up
We went over the main areas where Computer Vision in manufacturing adds great value. Of course, it takes investing in good quality costs and knowing your processes in full to see where to improve.
By now, it's clear that the ROI of predictive maintenance, catching defects early, automating inspection, and optimizing logistics far outweighs the effort required.
For a project to succeed, manufacturers also need to explain their needs clearly to computer vision experts. That can be hard.
At Pento, we are lucky to have team members from many backgrounds, including Process and Industrial Engineers. They bring both worlds together with their computer vision skills to craft tailored solutions for the needs of a manufacturer client, as part of our broader AI for manufacturing practice.
Are you looking for computer vision solutions for your manufacturing business? Contact us. We can bring you a step closer to your goals and help you become a Lighthouse of the industry.